- Hospital Furniture
- Neonatal Care Product
- Operating Surgical Tables
- Orthopedic Implants
- Surgical Operating Led Lights
- Orthopedic External Fixators
- Laryngoscopes
- Orthopaedic Power Tools
- Medical Disposables
- Hospital Clothing
- Anaesthesia Products
- Autoclaves & Sterilizers
- Hospital Holloware
- Suction Units
- Rehabilitation Aids
- Stethoscopes
- Anesthesia Machine & Ventilators
- Cold Chain Equipment
- Electro Medical Equipments
- Orthopedic Instruments
- Surgical Operating Led Lights
- Physiotherapy products
2026 Best Roll Thread Machine Types for Global Buyers
Choosing the right roll thread machine in 2026 requires more than comparing prices and motor power. Global buyers must examine thread size, material compatibility, production volume, automation level, and after-sales support. A compact machine may suit a small workshop, while a high-output model needs stable power, trained operators, and reliable tooling.
Details matter. This guide introduces major machine types for different manufacturing conditions. It considers flat-die, cylindrical-die, planetary, and CNC-controlled designs. Each type forms threads differently and serves specific workpieces. Steel fasteners, automotive parts, construction hardware, and precision components may require different pressure settings and die configurations. Practical selection should also include cycle time, changeover effort, dimensional accuracy, safety guarding, and spare-part availability.
Specifications can look impressive on paper. Real performance may differ. Buyers should request sample testing, inspection records, and clear warranty terms before placing an order. Supplier experience also matters, especially when installation, operator training, or remote troubleshooting is required across borders. Certifications should be checked against the destination market, not accepted blindly. No guide removes every uncertainty. Even experienced buyers can overlook shipping damage, voltage differences, or local maintenance limits.
This overview provides a practical starting point for evaluating the best roll thread machine types for global purchasing decisions. It combines technical considerations with real factory concerns, helping readers compare machines with greater confidence. Fit comes first. Reliability matters more than advertising.
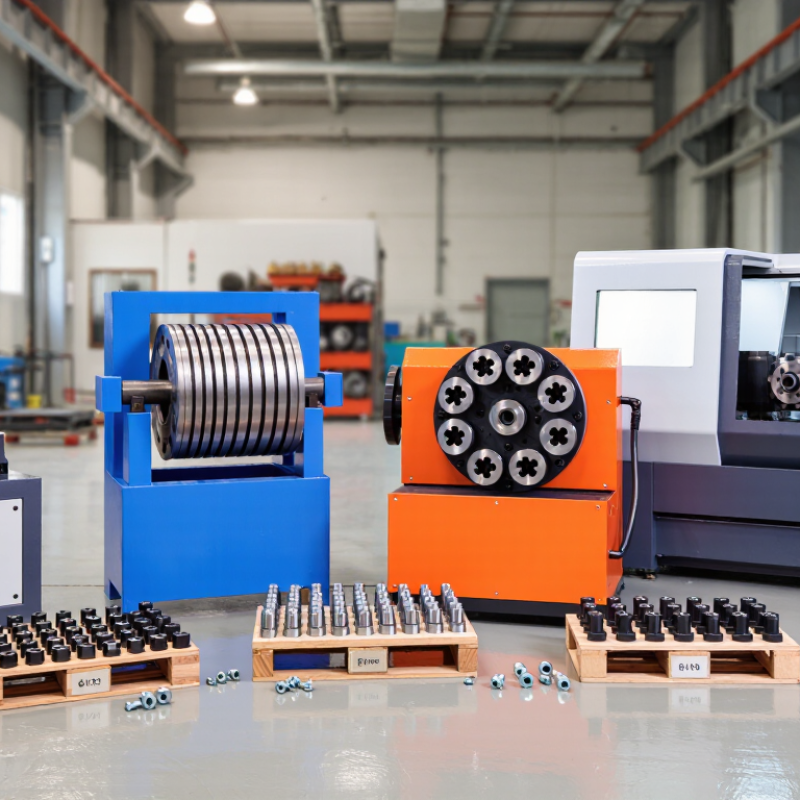
Table of Contents [Hide]
What Is a Roll Thread Machine and How Does It Work?
A roll thread machine forms threads by pressing hardened dies against a rotating metal blank. Unlike cutting, it displaces material instead of removing it. The blank rotates between two or more dies, while pressure pushes metal into the thread profile. The process can improve grain flow, surface hardness, and thread strength when speed, lubrication, and blank diameter are correctly matched. ISO 898-1 remains a useful reference when buyers evaluate mechanical properties for fastener applications.
The machine type matters.
Flat-die models suit high-volume production and simple cylindrical parts. Planetary machines handle continuous output with compact layouts. Two-die cylindrical systems offer flexibility for different diameters and shorter production runs. A technician should check die alignment, spindle speed, feeding accuracy, and cooling before judging capacity. Small errors leave visible double marks.
Industry data gives useful context. The World Steel Association reported 1.892 billion tonnes of crude steel production worldwide in 2023, showing the scale of the metalworking supply base. Grand View Research has also identified automation and precision forming as major drivers in the global metal forming equipment market. These figures do not guarantee machine performance. They only show strong industrial demand.
In practice, rolled threads may reduce scrap because chips are not produced. Yet this advantage is sometimes overstated. Hard alloys, poor lubrication, or incorrect preform sizing can cause die wear and unstable results. Buyers should request sample trials, dimensional reports, and cycle-time records before placing an order. A polished brochure is not proof.