- Hospital Furniture
- Neonatal Care Product
- Operating Surgical Tables
- Orthopedic Implants
- Surgical Operating Led Lights
- Orthopedic External Fixators
- Laryngoscopes
- Orthopaedic Power Tools
- Medical Disposables
- Hospital Clothing
- Anaesthesia Products
- Autoclaves & Sterilizers
- Hospital Holloware
- Suction Units
- Rehabilitation Aids
- Stethoscopes
- Anesthesia Machine & Ventilators
- Cold Chain Equipment
- Electro Medical Equipments
- Orthopedic Instruments
- Surgical Operating Led Lights
- Physiotherapy products
7 Best Core Pins Suppliers for Global Buyers?
Choosing the right Core Pins supplier can influence mold life, product quality, and production stability. A poor fit may create burrs, premature wear, or repeated tooling adjustments. For global buyers, the decision involves more than comparing unit prices. Steel grade, dimensional tolerance, heat treatment, surface finish, and inspection methods all matter.
This guide examines seven Core Pins suppliers serving international manufacturers and tooling companies. Each supplier is considered through practical purchasing criteria, including material traceability, customization capability, sample support, minimum order quantities, and delivery communication. Clear drawings and reliable tolerance data are essential. A supplier should also explain its quality process without hiding behind vague claims. Small details matter, such as protective packaging, thread protection, and readable inspection reports.
A polished website proves little.
Real confidence comes from consistent samples, responsive engineers, and documented production controls. Buyers should confirm whether pins suit cold runner molds, hot runner systems, die casting tools, or precision plastic molds. Regional availability can also affect freight costs, replacement speed, and technical support. Certifications may help, but they should be verified against actual production practices.
No supplier is perfect for every application. Some offer excellent customization but longer lead times. Others provide fast standard sizes but limited engineering assistance. This comparison is a starting point, not a substitute for technical review. Before placing an order, request drawings, material certificates, tolerance details, and a sample inspection. Careful verification may feel slower, but it usually prevents expensive tooling problems later.
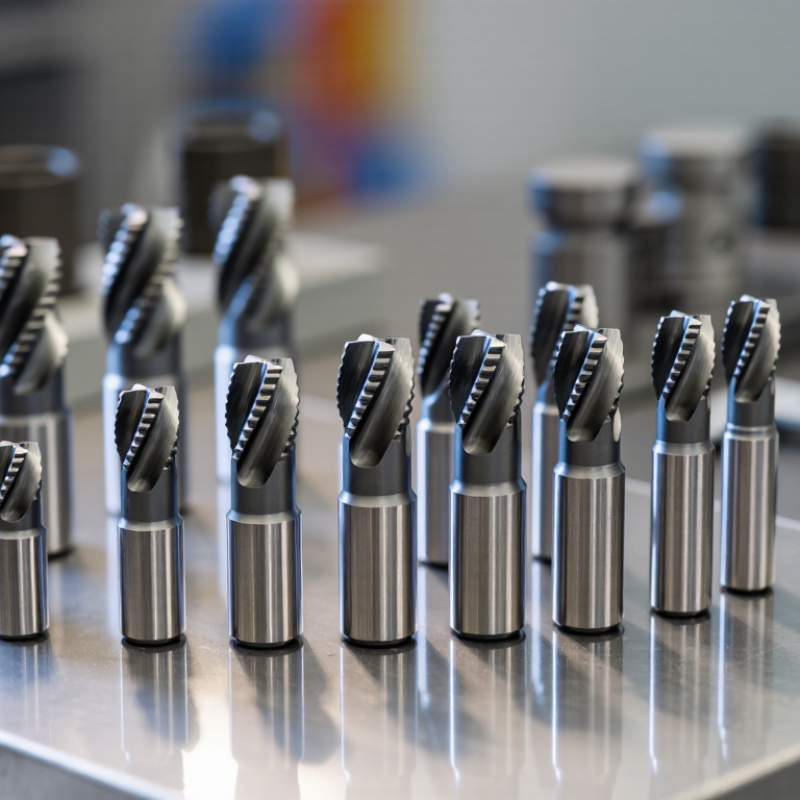
Table of Contents [Hide]
Core Pin Fundamentals: Materials, Sizes, and ±0.005 mm Tolerance Benchmarks
Core pins look simple, but their performance depends on material, geometry, and inspection discipline. Hardened tool steel suits high-volume molding because it resists wear and repeated thermal cycling. Stainless steel can be preferable when corrosion or demanding cooling conditions matter. Carbide offers excellent stiffness, yet it costs more and can fracture under shock loads. Material choice should match resin abrasiveness, mold temperature, and expected production volume.
Sizes must be specified beyond diameter. Buyers should confirm pin length, head style, fit length, and the working-end profile. A 2 mm pin may need a ground diameter, not only a nominal drawing value. Small errors become visible around ejector marks and thin ribs. Very short.
A practical benchmark for precision core pins is ±0.005 mm on critical diameters. This tolerance is meaningful only when linked to a datum, measurement method, and temperature-controlled inspection area. Coordinate measuring machines can verify location, while calibrated micrometers often check accessible diameters. Global buyers should request inspection reports, material certificates, hardness data, and sample approval records. Also review packaging; an unprotected tip can lose accuracy before installation.
In production trials, fit should be checked with the actual mold plate, not a loose gauge alone. That lesson is easy to overlook. Some suppliers advertise tight tolerances but leave roundness, straightness, or surface finish undefined. I would challenge that assumption. A reliable supplier explains process capability, identifies critical dimensions, and reports nonconforming results honestly. One imperfect sample should trigger investigation, not silent replacement.
7 Best Core Pins Suppliers for Global Buyers? - Core Pin Fundamentals: Materials, Sizes, and ±0.005 mm Tolerance Benchmarks
| Profile | Typical production region | Common core-pin materials | Typical diameter range | Typical length range | Standard dimensional capability | Fine capability benchmark | Typical surface finish | Best-fit applications |
|---|---|---|---|---|---|---|---|---|
| Profile 01 | East Asia | SKD61 / H13, SKH51 / M2, stainless tool steel | Ø0.50–25.00 mm | 10–300 mm | ±0.010 mm | ±0.005 mm on qualified dimensions | Ra 0.20–0.40 µm | High-volume injection molds and precision inserts |
| Profile 02 | Central Europe | H13, M2, powder-metallurgy tool steel | Ø1.00–32.00 mm | 20–450 mm | ±0.008 mm | ±0.005 mm for ground diameters | Ra 0.15–0.30 µm | Automotive, engineering plastics, and extended-life tooling |
| Profile 03 | South Asia | SKD61 / H13, D2, stainless steel | Ø0.80–20.00 mm | 15–250 mm | ±0.015 mm | ±0.005 mm by centerless grinding and inspection | Ra 0.25–0.50 µm | Custom prototypes, replacement pins, and medium-volume molds |
| Profile 04 | North America | H13, M2, 420 stainless steel | Ø1.50–38.00 mm | 25–500 mm | ±0.010 mm | ±0.005 mm subject to drawing review | Ra 0.20–0.40 µm | Low-volume precision work and rapid replacement parts |
| Profile 05 | Southeast Asia | H13, M2, 420 stainless steel | Ø0.60–25.00 mm | 10–350 mm | ±0.010 mm | ±0.005 mm on diameter and selected lengths | Ra 0.20–0.40 µm | Consumer products, electronics, and general molding |
| Profile 06 | East Asia | SKD61 / H13, SKH51 / M2, carbide | Ø0.20–12.00 mm | 5–180 mm | ±0.008 mm | ±0.003–0.005 mm for micro-diameter pins | Ra 0.10–0.25 µm | Micro molding, medical components, and connector tooling |
| Profile 07 | Eastern Europe | H13, D2, corrosion-resistant tool steel | Ø1.00–30.00 mm | 20–400 mm | ±0.012 mm | ±0.005 mm after grinding and final verification | Ra 0.20–0.45 µm | Industrial molds, repair programs, and corrosion-sensitive applications |
| Dimension or specification | Common benchmark | Why it matters | Recommended buyer check |
|---|---|---|---|
| Material hardness | H13 after heat treatment: approximately 44–52 HRC; M2: approximately 58–64 HRC | Controls wear resistance, toughness, and resistance to deformation | Request hardness results and heat-treatment condition |
| Diameter tolerance | General: ±0.010–0.015 mm; precision: ±0.005 mm | Affects mold alignment, venting, flash, and pin movement | Identify whether the tolerance applies to the full length or only the working section |
| Straightness | Approximately 0.01–0.03 mm per 100 mm for precision ground pins | Reduces binding, uneven wear, and premature breakage | Specify the inspection length and measurement method |
| Surface roughness | Ra 0.10–0.40 µm for ground working surfaces | Influences friction, ejection force, wear, and molded-part appearance | Confirm whether the Ra value is for the tip, body, or complete working area |
| Diameter selection | Common production sizes: Ø1–10 mm; micro pins may be below Ø0.50 mm | Smaller pins improve design flexibility but are more sensitive to buckling and breakage | Check unsupported length, ejection load, and minimum wall thickness |
| Tip geometry | Flat, stepped, radius, tapered, or custom-form tips | Determines part contact, stress concentration, and visible ejector marks | Provide a dimensioned drawing with angular, radius, and edge-break details |
| Coating option | Common PVD coating thickness: approximately 1–5 µm | Can improve wear resistance and reduce adhesion in demanding molding conditions | Account for coating thickness in final diameter and fit calculations |
| Inspection evidence | Dimensional report, hardness report, material certificate, and surface-finish record | Provides traceability for ±0.005 mm requirements and batch acceptance | Require calibrated gauges, sampling plan, and agreed acceptance criteria |
Note: ±0.005 mm is a precision benchmark rather than a universal standard. Actual capability depends on material, diameter-to-length ratio, heat treatment, grinding process, geometry, inspection temperature, and the specific tolerance stated on the engineering drawing.