- Hospital Furniture
- Neonatal Care Product
- Operating Surgical Tables
- Orthopedic Implants
- Surgical Operating Led Lights
- Orthopedic External Fixators
- Laryngoscopes
- Orthopaedic Power Tools
- Medical Disposables
- Hospital Clothing
- Anaesthesia Products
- Autoclaves & Sterilizers
- Hospital Holloware
- Suction Units
- Rehabilitation Aids
- Stethoscopes
- Anesthesia Machine & Ventilators
- Cold Chain Equipment
- Electro Medical Equipments
- Orthopedic Instruments
- Surgical Operating Led Lights
- Physiotherapy products
How to Choose an Automatic Price Labelling Machine
Choosing an Automatic Price Labelling Machine is not simply a matter of selecting the fastest model. It is a production decision involving accuracy, product handling, operator safety, and long-term maintenance. A machine may label 120 products per minute, yet perform poorly with uneven packages or dusty surfaces.
Mike Fairley, a respected label-industry educator, offers a useful principle: “A label only succeeds when it performs reliably on the product and on the production line.” This practical view keeps the buying process grounded. The machine must match your package shapes, label dimensions, adhesive type, and daily output. It should also communicate smoothly with weighing systems, barcode printers, conveyors, or existing filling equipment.
Small details matter. A photoelectric sensor should detect dark and transparent packages accurately. The applicator should place each label without wrinkles or edge lifting. Operators need clear controls, quick changeovers, and easy access to rollers. They also need simple cleaning procedures.
Do not trust speed alone.
A proper evaluation includes sample testing with real products and labels. Ask suppliers to demonstrate performance during start-stop operation, product gaps, and roll changes. Check spare-part availability, training, warranty coverage, and service response times. These points often receive less attention before purchase.
The ideal Automatic Price Labelling Machine is not always the most advanced model. Sometimes, a simpler unit offers better reliability and lower ownership costs. That judgment can be imperfect. Production conditions change, and initial assumptions may prove wrong. A careful comparison, supported by trial results and operator feedback, creates a more dependable investment.
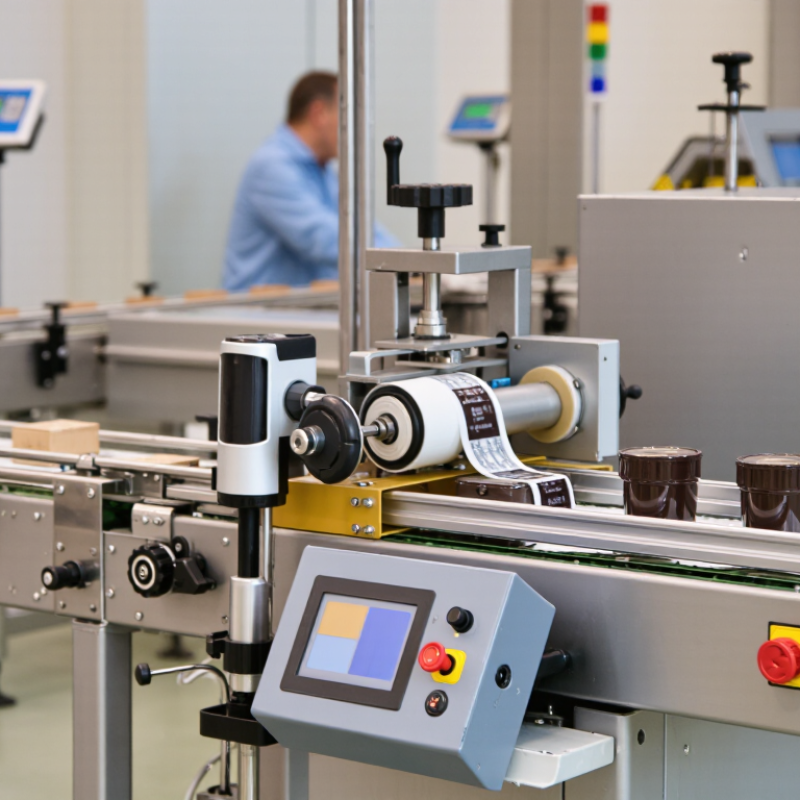
Table of Contents [Hide]
What Is an Automatic Price Labelling Machine?
An automatic price labelling machine applies printed price labels to products with limited manual handling. It may combine a printer, label dispenser, sensor, conveyor, and control system. Some models also connect to a weighing unit, creating a price from measured weight. The machine reads product position, prints variable information, and places the label at a defined location. In practice, it is a small data-and-motion system, not simply a faster sticker applicator.
The need is growing with packaging automation. Grand View Research valued the global packaging machinery market at about US$52.83 billion in 2023 and projected a 5.8% annual growth rate from 2024 to 2030. This broader figure includes labelling equipment, but it shows the industrial direction clearly. PMMI reports that labour availability, line flexibility, and traceability remain important packaging investment drivers. A suitable machine should therefore support different package sizes, label materials, and production speeds.
Look closely at the details.
A machine that labels 80 packs per minute may perform poorly with wet surfaces or uneven trays. Test real products, including damaged cartons and changing label rolls. Ask for evidence on placement accuracy, printer resolution, changeover time, and rejected labels. One overlooked issue is data control. Incorrect prices can spread quickly across a production run. The best choice is not always the fastest machine; it is the one operators can adjust, inspect, and maintain without confusion.
How to Choose an Automatic Price Labelling Machine - What Is an Automatic Price Labelling Machine?
| Evaluation Dimension | Typical Data or Specification | What It Means | Selection Guidance |
|---|---|---|---|
| Machine Function | Automatically dispenses and applies price, barcode, weight, batch, or promotional labels to products or packages. | It reduces manual labelling work and helps keep label placement consistent. | Choose a system that supports the required label content and package type. |
| Labelling Method | Common methods include pressure-sensitive label application, top labelling, side labelling, wrap-around labelling, and print-and-apply labelling. | The method determines where and how the label is attached. | Match the method to the product shape, surface, and label position. |
| Typical Operating Speed | Approximately 20–120 products per minute, depending on product size, label position, conveyor layout, and inspection requirements. | Speed indicates the expected production capacity. | Select a rated speed at least 15–25% above the normal production target. |
| Label Application Accuracy | Typical placement accuracy is approximately ±1–3 mm under stable product presentation and conveyor conditions. | Higher accuracy improves appearance and barcode readability. | Request a sample test using the actual products and labels before purchase. |
| Product Size Compatibility | Many general-purpose systems handle products approximately 30–300 mm wide and 20–250 mm high, subject to machine design. | Product dimensions affect conveyor stability, sensor detection, and label positioning. | Confirm the minimum and maximum product dimensions, weight, and shape. |
| Label Size Range | A commonly supported range is about 20–150 mm in label width and 15–250 mm in label length. | The label roll and applicator must accommodate the required dimensions. | Check label material, gap size, roll diameter, core diameter, and winding direction. |
| Label Material | Typical materials include coated paper, direct-thermal paper, thermal-transfer stock, polypropylene, and polyethylene labels. | Material selection affects durability, moisture resistance, print quality, and adhesion. | Use moisture-resistant synthetic labels for refrigerated, frozen, or wet environments. |
| Printing Capability | Systems may apply preprinted labels or print variable information such as price, weight, date, lot number, and barcode before application. | Variable printing supports changing product and pricing information. | Choose print-and-apply equipment when each product requires unique data. |
| Barcode Support | Common formats include EAN-13, UPC-A, Code 128, QR Code, and Data Matrix, subject to printer and software compatibility. | Correct barcode generation and placement support scanning at checkout and throughout the supply chain. | Verify the required barcode format, print resolution, contrast, and inspection process. |
| Product Detection | Photoelectric sensors, spacing sensors, encoder feedback, and optional vision systems are commonly used. | Detection controls the timing and position of label application. | Use vision inspection when label presence, position, or printed data must be verified. |
| Conveyor Integration | Typical conveyor speeds range from approximately 5–30 m/min, depending on product and line configuration. | Stable product movement is essential for accurate application. | Confirm conveyor height, direction, spacing, speed control, and connection points. |
| Changeover Time | Manual changeovers commonly take approximately 5–20 minutes, depending on product and label format. | Shorter changeovers reduce downtime when multiple products are processed. | Look for tool-free adjustments, stored recipes, guides, and clear adjustment scales. |
| Control System | Typical controls include a touchscreen interface, programmable recipes, speed adjustment, alarm history, and sensor status display. | The control system affects ease of operation and troubleshooting. | Choose an interface with password levels, multilingual support, and easy recipe management. |
| Electrical Requirements | Many systems use single-phase or three-phase power between 100–240 V, with total consumption often below 1.5 kW excluding connected equipment. | Power requirements must match the installation site. | Confirm voltage, frequency, phase, plug type, compressed-air needs, and available utilities. |
| Operating Environment | Typical operating temperatures are approximately 5–40°C, with optional designs for dusty, humid, or washdown areas. | Temperature, moisture, and dust can affect adhesive performance and electronic components. | Specify the cleaning method, humidity, temperature range, and hygiene requirements. |
| Machine Construction | Stainless-steel or anodized-aluminum frames are commonly used; stainless steel is preferred for food, beverage, and washdown applications. | Construction materials influence durability, corrosion resistance, and cleanability. | Select hygienic construction when the machine is installed near exposed food or wet processing areas. |
| Safety Features | Common features include emergency-stop buttons, guarded moving parts, interlocked covers, overload protection, and low-label alarms. | Safety functions protect operators and help prevent equipment damage. | Review applicable local machine-safety requirements and perform a site risk assessment. |
| Data and System Integration | Possible interfaces include Ethernet, USB, serial communication, digital I/O, database connections, and production-line signals. | Integration enables automatic transfer of product, price, weight, and traceability information. | Confirm communication protocols and data ownership with the existing production or retail system. |
| Maintenance Requirements | Routine tasks include cleaning sensors, checking rollers, inspecting belts, removing adhesive buildup, and replacing worn applicator parts. | Regular maintenance supports consistent application and reduces unplanned downtime. | Ask for preventive-maintenance intervals, spare-parts lists, service access, and operator training. |
| Best-Fit Application | Suitable for packaged food, retail products, cartons, boxes, bottles, containers, and other uniform items requiring repeatable labels. | Automatic labelling provides the greatest benefit when product flow is regular and label information is standardized or digitally controlled. | Choose semi-automatic equipment for low-volume or irregular production and fully automatic equipment for continuous, higher-volume lines. |